

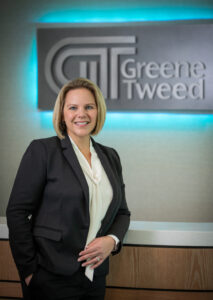
 Magen Buterbaugh was appointed President and CEO of Greene Tweed in January 2023. A seasoned leader, with broad industry expertise, Magen has led multiple chemicals & materials-based businesses – spanning from startups to multibillion-dollar enterprises. She led and scaled new innovative research and development platforms and step-changed growth across multiple commercial organizations, while transforming organization effectiveness.
Known for her passion for chemicals and innovative materials, Magen’s leadership inspires Greene Tweed to continue to be the market-leading innovator in high-end elastomers, thermoplastics, composites, and sealing solutions.
Over her 20-year career, Magen has played a pivotal role in championing innovation and seizing opportunities for growth. Before joining Greene Tweed, Magen led the global commercial, product, technology, and regulatory affairs organizations at DCL Corporation, a global manufacturer and supplier of high-quality colored pigments for the coatings, plastics, and ink industries. Previously, Magen steered DuPont’s (and then subsequently Chemours) Global Fluorochemicals business. She held numerous other positions with DuPont leading cross-functional teams in various positions, including capital engineering, operations, strategic planning, commercial and business management roles across various business units.
Magen currently serves on the Board of Directors for PQ Corporation as well as the National Association of Manufacturers. She is also a member of the 2024-2026 cohort of Advancing Women Executives sponsored by McKinsey, an initiative to increase the portion of women in executive roles.
Tell us about your company?
Greene Tweed is a 160-plus-year-old, fourth-generation family-owned company specializing in high-performance materials and engineered components for the world’s most demanding applications. We design and manufacture advanced sealing solutions, thermoplastics, composites, and other highly engineered components that are built to perform in environments where failure simply isn’t an option. We primarily serve the semiconductor, aerospace & defense, energy, industrial operations and life sciences industries.
What makes us unique is the combination of materials science, engineering expertise, and close customer collaboration. Our engineers work directly with customers to understand the application, environment, and challenge they are trying to solve, and then develop a solution tailored to those needs.
What problems are you solving?
In semiconductor, our customers are being asked to do more under difficult operating conditions. As chip architectures become more complex, manufacturing processes become more demanding, with greater exposure to aggressive chemistries and extreme conditions, like high temperatures. At the same time, fabs are intensely focused on reliability, contamination control, productivity, and yield.
Greene Tweed engineers materials and components that solve these challenges across the full spectrum of chip manufacturing. In front-end manufacturing, we address plasma resistance, extreme thermal performance, and contamination control in processes like Etch, ECD, and CMP. In Etch, seals must deliver strong plasma resistance and low particulation. In ECD, they must withstand aggressive plating acids. In CMP, they must resist abrasive slurries and mechanical wear. Greene Tweed’s Chemraz® seals are engineered to meet these challenges where traditional elastomers struggle.
The shift toward advanced packaging, driven in part by surging AI demand, is also creating new sealing challenges. Hybrid bonding, glass substrates, panel-level packaging, and co-packaged optics are introducing larger form factors, complex multi-die systems, and unprecedented cleanliness requirements. With glass substrates, we seal much larger surface areas where warpage and shifting mechanical stresses are critical concerns. In co-packaged optics, even trace outgassing can compromise optical clarity. Our ultra-low outgassing, high-purity Chemraz® materials provide stable, low-force sealing that protects fragile components while maintaining system integrity.
What application areas are your strongest?
We primarily serve semiconductor, aerospace and defense, energy, chemical processing and life sciences industries. The common denominator is that these are highly demanding applications where reliability matters and failure can have significant consequences. We’re working with the world’s leading companies in these industries to custom design and engineer components for their specific high-performance requirements and applications.
Within semiconductor specifically, Greene Tweed sealing solutions are used across all major semiconductor manufacturing processes, including etch, deposition, cleaning and stripping, electrochemical deposition, advanced packaging, CMP, lithography, and subfab systems. In these environments, seals must withstand combinations of plasma, aggressive chemistries, high temperatures, thermal cycling, and contamination control requirements.
One of our core strengths is high-performance sealing solutions, including our Chemraz® FFKM portfolio, for critical semiconductor processing environments. Our experience with advanced materials allows us to support customers in applications involving aggressive chemistries and extreme operating conditions. We also see opportunities emerging as semiconductor processes evolve, including areas such as advanced packaging.
What keeps your customers up at night?
Reliability. For semiconductor customers, even the smallest component can have an outsized impact. If that component doesn’t perform as expected, the downstream consequences can be major.
Customers are also thinking about yield, contamination, equipment uptime, supply-chain resilience, speed of innovation, and more recently, sustainability. They’re trying to anticipate what the next generation of semiconductor manufacturing is going to require from their equipment and materials.
That’s why we value collaborative partnerships so much. The best time to solve a materials challenge isn’t after something fails. It’s working together early enough in the development process to understand what the next application will demand and engineer for it.
Greene Tweed has always delivered high quality, high-performance engineered components using our Chemraz® FFKM product line for the semiconductor industry’s harshest applications. We have also worked with our customers on supply chain resilience to support their growth by investing in our global manufacturing footprint including our new facility in Korea & continuing to expand production in Taiwan as well as supply from multiple US sites.
What does the competitive landscape look like and how do you differentiate?
There are a number of very capable advanced-materials and engineered-component companies in the market. However, I’m much more interested in what our customers need from us and whether we’re solving the problems that matter most to them.
Where I think Greene Tweed differentiates itself most is in the combination of materials expertise, application engineering, global manufacturing capability and capacity, and customer relationships. Because our approach is highly technical and collaborative, our teams develop a deep understanding of the customer’s application, rather than simply supplying a component.
With mission-critical applications, performance has to be considered over the full life of the component. Our customers are thinking about reliability, qualification, service life, and consistent performance under extreme conditions. That’s the standard we engineer toward.
What new features/technology are you working on
A lot of our innovation starts with where our customers are going next rather than what we can sell them today.
In semiconductors, we are looking at the increasingly demanding environments created by more advanced chip architectures and processes. That involves continuing to advance materials capable of performing under extreme chemical and thermal conditions while supporting the industry’s expectations around productivity and performance. We’re also looking closely at emerging opportunities such as advanced packaging, where precision-engineered components and materials will become critical.
Beyond semiconductors, we’re advancing our capabilities in thermoplastic composites, high-performance sealing technologies, precision manufacturing, automation and faster prototyping. Across all of it, the goal remains anticipating where the customer’s technology is going and making sure our materials and engineering capabilities are ready to help them get there.
How do customers normally engage with your company?
Our model is predominantly direct because of the highly engineered nature of what we do. We want our commercial and engineering teams close to the customer and close to the application.
Typically, that begins with a performance challenge or a new requirement. Our teams work with the customer to understand the operating environment, what they are trying to achieve, and what isn’t working with the current solution. From there, we bring together our materials science, design and application engineering capabilities to develop the right solution.
Greene Tweed has locations across the world, including operations in the U.S., Korea, Taiwan, the U.K. and Switzerland, along with regional sales and technology resources in multiple global locations. That footprint allows us to combine global manufacturing, technology and engineering capabilities with the local support customers expect.
Contact Greene Tweed
Also Read:
CEO Interview with Vivek Raghuraman of Mixx Technologies
CEO Interview with Dr. Stefan Pastine of Thintronics
CEO Interview With Nick Kurayev of ScienceSoft
Share this post via:


Comments
There are no comments yet.
You must register or log in to view/post comments.